Epoxy Panel Roving: Why Structural FRP Panels Out‑perform When You Choose This Specialized Reinforcement
Table of Contents
Add a header to begin generating the table of contents
Introduce
Many structural FRP panel defects such as surface pinholes, poor inter‑laminar strength and delamination stem not from resin quality, but from mismatched glass reinforcement.
General‑purpose panel roving works fine for polyester‑matrix panels, yet delivers weak bonding, slow wet‑out and low mechanical values when paired with amine‑cured epoxy. That is whyEpoxy Panel Rovingexists as dedicated reinforcement for high‑performance epoxy‑based structural panels.
What Is Epoxy Panel Roving?
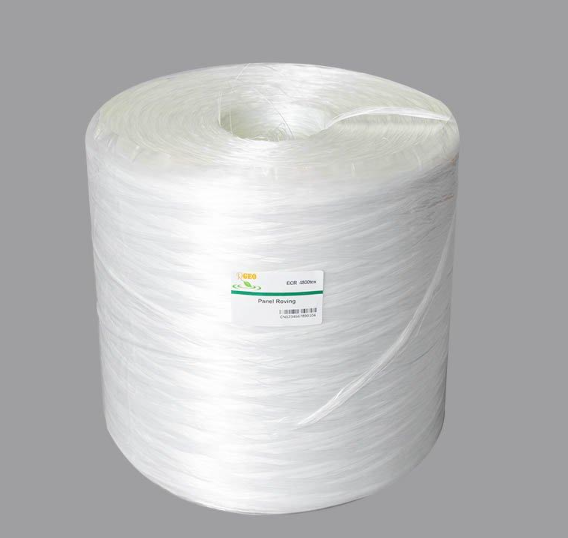
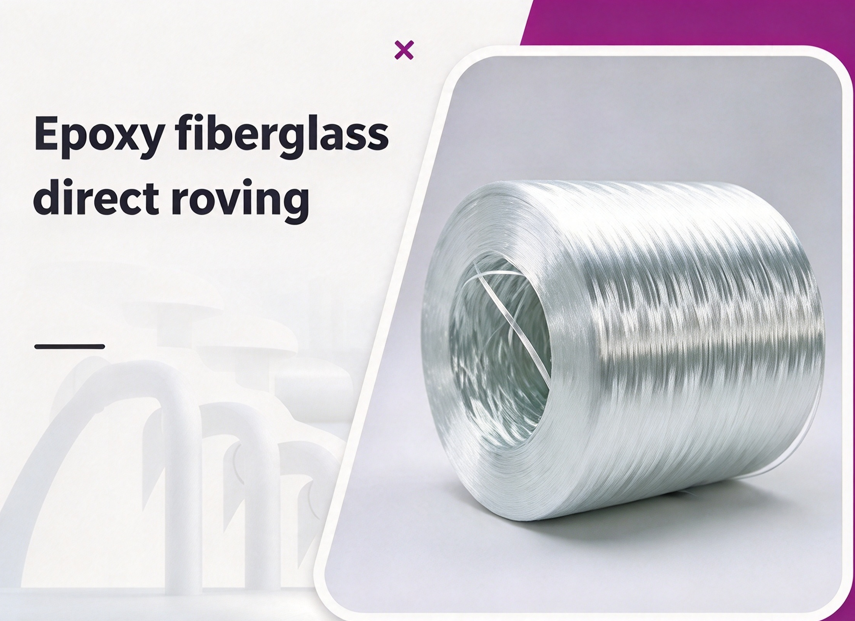
Epoxy Panel Roving is continuous E‑glass roving optimized for flat panel production. Its core distinction from ordinary roving lies in silane sizing formulation: the coating is chemically matched to amine‑cured epoxy resin instead of methacrylate sizing for unsaturated polyester.
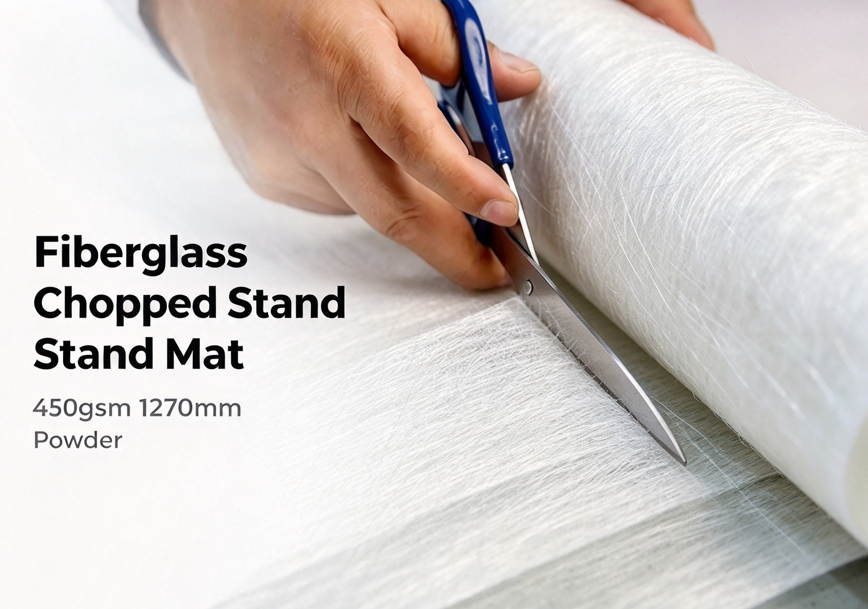
Typical tex range covers 1200 tex to 4800 tex, selected according to panel thickness, production speed and resin viscosity.
Even premium E‑glass cannot achieve target inter‑laminar shear strength without correct surface treatment.Epoxy Panel Rovingsolves fiber‑resin interface failure risk for epoxy composite panels.
Main Manufacturing Processes for Epoxy Panel Roving
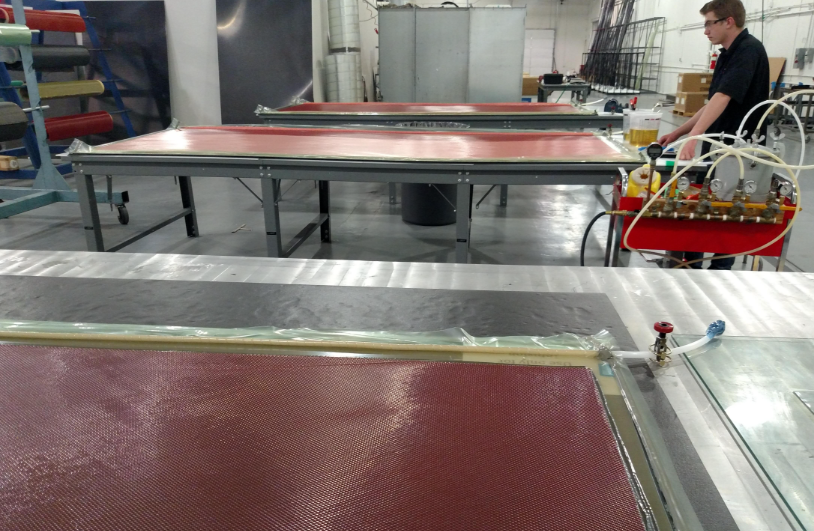
Epoxy Panel Rovingsupports three mainstream panel production workflows, vacuum infusion being its most widely‑adopted process.
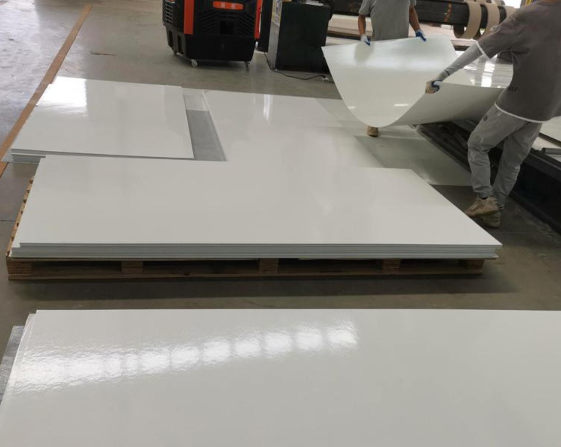
In vacuum infusion, multiple roving strands are laid as dry reinforcement stack, then epoxy resin flows through the preform under vacuum pressure to form large‑size flat panels.
In hand lay‑up, operators impregnate Epoxy Panel Roving‑derived woven roving with epoxy manually for small‑batch customized panels.
In pultrusion, rovings pass through epoxy resin bath and heated die to make constant‑cross‑section panel substrates and grating profiles.
Stable strand integrity, continuous high‑speed production
Epoxy Panel Roving vs General‑Purpose Panel Roving
Performance gaps between Epoxy Panel Roving and general‑purpose roving come entirely from sizing chemistry, not glass filament itself.
General‑purpose roving uses methacrylate‑based sizing designed for styrene‑containing polyester and vinyl‑ester resin systems; when processing epoxy panels, it causes slow wet‑out, micro dry spots and decreased inter‑laminar shear strength.
Epoxy Panel Roving adopts glycidoxy silane sizing to create stable chemical coupling between glass surface and amine‑hardened epoxy matrix.
Why Sizing Chemistry Determines The Performance of Epoxy Panel Roving
The surface coating onEpoxy Panel Roving fulfills three critical tasks: protect glass filaments from abrasion during unwinding and lay‑down, minimize fuzz for clean preform stacking, and build chemical bonding between inorganic glass and organic epoxy matrix.
Even high‑quality E‑glass will produce delamination‑prone panels if sizing is incompatible with amine curing agent. Qualified suppliers ofEpoxy Panel Roving need to provide test data proving amine‑epoxy compatibility, instead of simply marking “epoxy compatible” on datasheets.
Key Parameters When Specifying Epoxy Panel Roving For FRP Panels
When producing large flat panels by vacuum infusion, Epoxy Panel Roving must unwind smoothly without broken filaments or heavy fuzz.
Fabricators should select tex value matching panel thickness and infusion flow rate. Too‑heavy tex reduces resin penetration; too‑fine tex lowers production efficiency. Moisture control is also critical forEpoxy Panel Roving.
Damp roving will introduce void defects inside epoxy panels and weaken long‑term anti‑corrosion performance.
Epoxy Panel Roving delivers stable fiber‑resin interfacial bonding for epoxy‑matrix FRP flat panels. Whether you produce vacuum‑infused marine deck panels, anti‑corrosion wall boards, electrical insulation plates or pultruded grating substrates, selecting properly‑sized Epoxy Panel Roving, instead of visually‑similar general‑purpose roving, is critical to avoid voids, delamination and early‑stage panel failure.
Always verify resin compatibility, tex specification and moisture‑proof packaging before bulk purchasing. Contact our team for samples, technical datasheets and grade recommendations.
Do you want to know the technical parameters and TDS of products?
You can leave the specifications and contact information you need~ Our technicians will immediately organize the exclusive information for you and send it to your email!
Interested in this specification?
You can leave your contact information here, and we will send you detailed specifications and application cases to make your purchase clearer~
Contact us via email
You can leave a message about the fiberglass and other composite materials you are interested in/looking for.
We will send you a clear quotation (including product price + shipping cost) within 12 hours.
How can we help you?
You can leave a message about the fiberglass materials you are interested in/looking for.
We will send you a clear quotation (including product price + shipping cost) within 12 hours.