Epoxy Fiberglass Direct Roving: Why High‑Pressure FRP Components Prefer It Over General‑Purpose Roving
Table of Contents
Add a header to begin generating the table of contents
Introduce
Many composite failures happen not from poor fiber strength, but from mis‑matched roving‑resin compatibility. General‑purpose glass roving performs well in polyester resin systems, yet often delivers low burst strength, fuzzing and poor wet‑out when paired with amine‑cured epoxy. That is why Epoxy Fiberglass Direct Rovingexists as a dedicated composite reinforcement for high‑stress epoxy FRP parts.
Core Production Processes for Epoxy Fiberglass Direct Roving
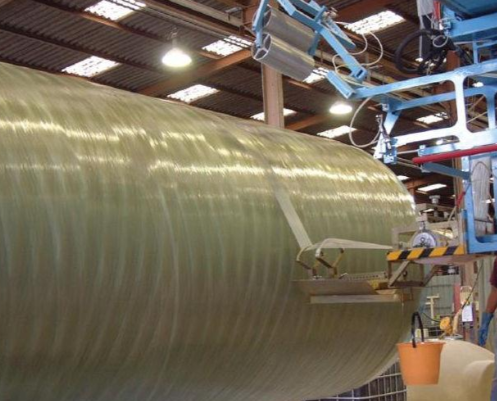
Epoxy Fiberglass Direct Roving fits three mainstream composite manufacturing workflows, with filament winding being its dominant application scenario. In filament winding, roving is pulled under precise tension and wound around rotating mandrels to form closed pressure‑bearing structures.
In pultrusion, multiple strands are pulled through epoxy resin bath and heated die for constant‑cross‑section structural profiles. It can also be woven into woven roving fabric for hand‑laid epoxy laminates.
Process
Typical Finished Product
Key Advantage of This Roving
Filament winding
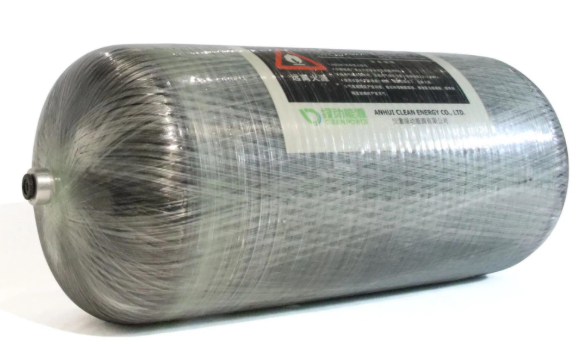
High‑pressure oil/water pipes, CNG cylinders, chemical pressure vessels
High burst & fatigue resistance, low fuzz under high tension
Epoxy Fiberglass Direct Roving vs General‑Purpose Direct Roving
Performance gap between Epoxy Fiberglass Direct Rovingand general‑purpose roving originates entirely from sizing chemistry, not glass filament itself.
General‑purpose roving uses methacrylate sizing optimized for styrene‑containing polyester/vinyl‑ester resins; when immersed in amine‑epoxy, wet‑out slows, interface bonding weakens and composite mechanical indexes drop significantly.
Epoxy Fiberglass Direct Roving adopts glycidoxy‑functional silane sizing to build stable covalent bonding with amine‑hardened epoxy matrix.
Feature
General‑Purpose Direct Roving
Epoxy Fiberglass Direct Roving
Target resin system
Unsaturated polyester, vinyl ester
Amine‑cured epoxy resin
Sizing chemistry
Methacrylate silane
Glycidoxy silane
Wet‑out performance in epoxy
Slow, dry‑spot risk
Fast, uniform impregnation
Fuzz under high winding tension
Noticeable
Low hairiness
Burst / fatigue performance in epoxy composite
Moderate
Optimized for pressure parts
Typical end‑use
Ordinary FRP tanks, panels
CNG cylinders, high‑pressure epoxy vessels
Why Sizing Formulation Defines Performance of Epoxy Fiberglass Direct Roving
The sizing coating onEpoxy Fiberglass Direct Rovingundertakes three core missions: protect glass filaments from abrasion during high‑speed pulling, prevent strand fuzzing under winding tension, and create chemical coupling between inorganic glass surface and organic epoxy matrix.
Even premium E‑glass cannot achieve design burst pressure if the sizing is incompatible with amine hardener. For this reason, qualified suppliers of Epoxy Fiberglass Direct Rovingmust provide test reports verifying compatibility with amine‑cured epoxy, instead of only marking “compatible with epoxy” on product sheets.
Key Factors When Specifying Epoxy Fiberglass Direct Roving for Filament Winding
When running filament‑winding lines, Epoxy Fiberglass Direct Rovingmust maintain stable strand feeding without snapping or excessive fuzz.
Operators need to match roving tex to mandrel dimension and winding speed. Too‑heavy tex leads to uneven band lay‑down; overly fine tex reduces production efficiency.
Moisture control is also critical for Epoxy Fiberglass Direct Roving. Damp bobbins destroy resin wet‑out and generate void defects in pressure‑bearing composite wall.
Recommended Tex Grades by End‑Product for Epoxy Fiberglass Direct Roving
Different finished components require different tex grades ofEpoxy Fiberglass Direct Roving. Thick‑wall pressure vessels and large‑diameter high‑pressure pipes normally adopt heavier 2400‑4800 tex to boost winding efficiency.
Thin‑wall CNG cylinders and small‑diameter pressure parts choose medium‑fine 1200‑2000 tex for precise wall‑thickness control. For pultruded insulating profiles and woven roving production, tex selection depends on die opening or weaving loom specification.
End‑Product
Suggested Tex Range
Main Process
CNG gas cylinders, thin‑wall pressure vessels
1200‑2400 tex
Filament winding
Large‑diameter high‑pressure epoxy pipes
2400‑4800 tex
Filament winding
Pultruded structural beams & grating
2400‑4800 tex
Pultrusion
Epoxy woven roving fabric
1200‑2400 tex
Weaving
FAQ About Epoxy Fiberglass Direct Roving
Q: Can I use general‑purpose direct roving with amine‑cured epoxy resin?
You can perform lab trials, but it is not allowed for pressure‑rated safety parts. Epoxy Fiberglass Direct Rovinguses glycidoxy silane sizing matching amine hardener; general‑purpose roving leads to poor interface bonding and degraded burst‑fatigue performance.
Q: What tex grade should I choose for CNG cylinder winding?
Most industrial CNG winding production lines adopt Epoxy Fiberglass Direct Rovingfrom 2400 tex to 4800 tex, balancing winding efficiency and wall‑thickness accuracy. Thin‑wall small‑size cylinders can shift down to 1200‑2000 tex.
Q: Does Epoxy Fiberglass Direct Roving work for pultrusion process?
Yes. Epoxy Fiberglass Direct Roving with low‑fuzz property is widely applied for epoxy‑matrix pultruded structural and insulating profiles.
In Conclusion
Epoxy Fiberglass Direct Roving delivers reliable fiber‑resin interfacial bonding for amine‑cured epoxy composite parts. For filament‑wound high‑pressure pipes, CNG cylinders, pressure vessels, pultruded profiles and woven fabrics, choosing correct sizing‑formulated Epoxy Fiberglass Direct Roving, rather than visually‑similar general‑purpose roving, is decisive for final burst strength and service life.
Always confirm resin compatibility, tex specification and moisture‑proof packaging before bulk procurement. Contact our team for samples, technical datasheets and grade recommendations.
Do you want to know the technical parameters and TDS of products?
You can leave the specifications and contact information you need~ Our technicians will immediately organize the exclusive information for you and send it to your email!
Interested in this specification?
You can leave your contact information here, and we will send you detailed specifications and application cases to make your purchase clearer~
Contact us via email
You can leave a message about the fiberglass and other composite materials you are interested in/looking for.
We will send you a clear quotation (including product price + shipping cost) within 12 hours.
How can we help you?
You can leave a message about the fiberglass materials you are interested in/looking for.
We will send you a clear quotation (including product price + shipping cost) within 12 hours.